


Rapid prototyping service for metal parts, without the tooling delay. Because laser cutting, bending and five-axis machining need no die, a first article can be produced from a drawing or a 3D model without cutting a tool first — which is the whole reason prototyping is fast here. Engineering responds within 3 hours on working days, and there is no minimum order quantity. ISO 9001:2015, registration 34025Q30296R0S.
| No tooling | part from drawing, no die required |
| ±0.005 mm | machined features |
| 12,000 W | fibre laser for flat profiles |
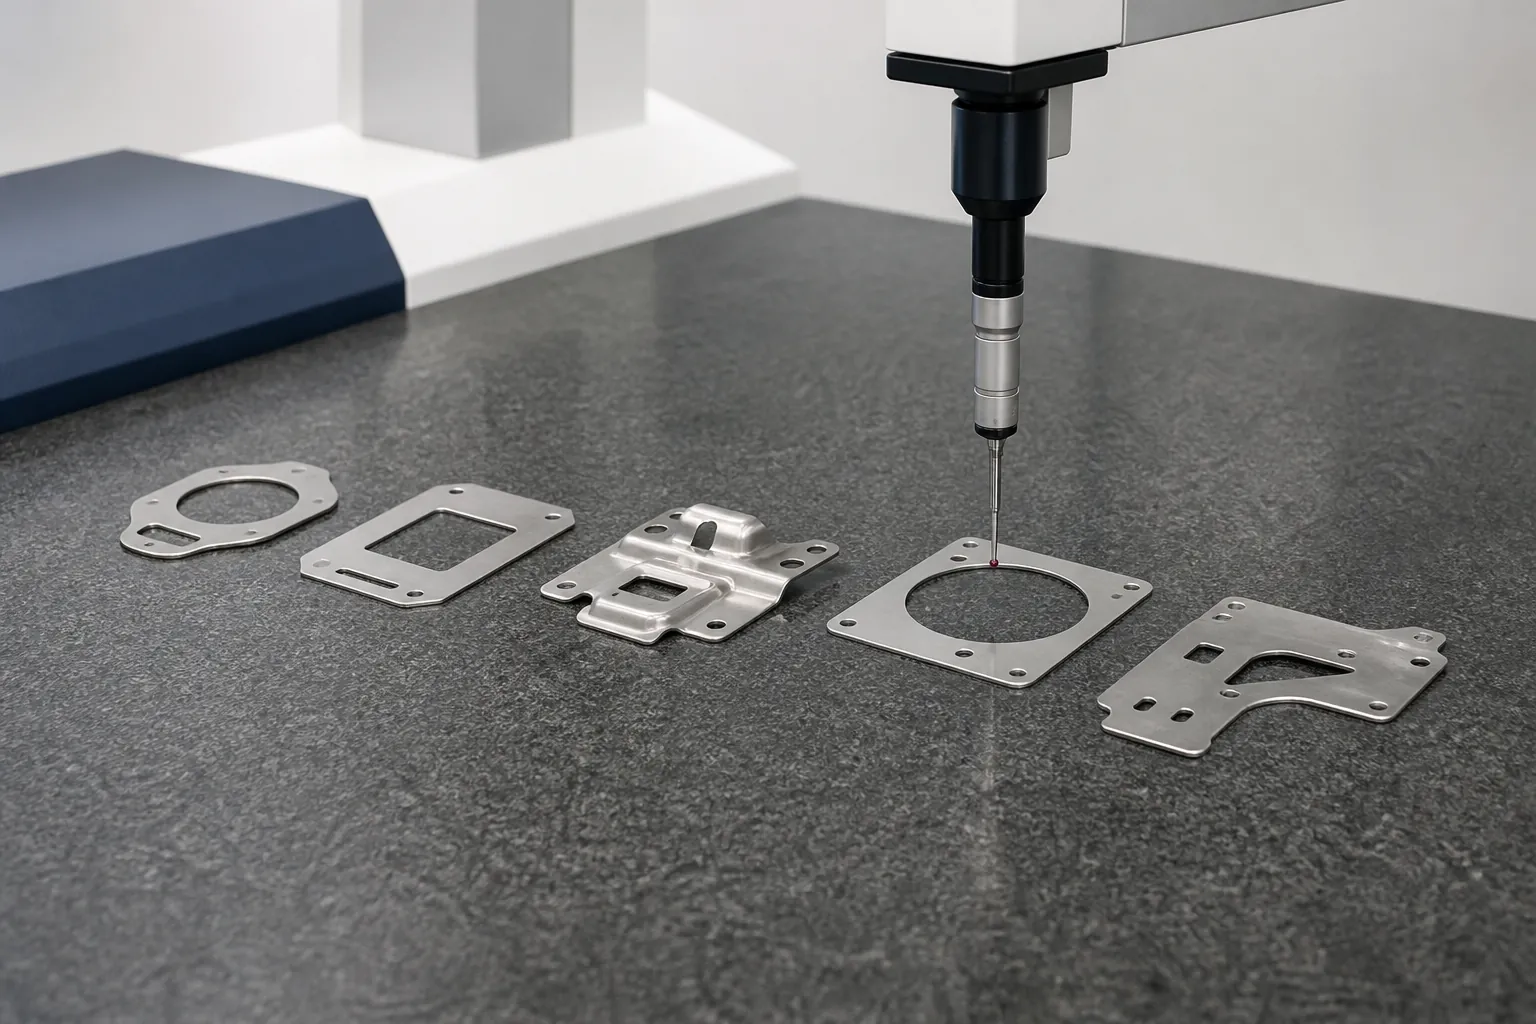
| CMM + FAI | first article reporting |
| No MOQ | one piece is a valid order |
| ISO 9001:2015 | reg. 34025Q30296R0S |
Why use us for prototyping
Nothing has to be cut first. A prototype from a die shop begins with a tool. Here it begins with your file: the profile is cut on the laser, the bends made on the press brake and any precision feature machined. That removes the longest lead time in the chain and the largest cost at the stage where the design is most likely to change.
You can revise and we re-cut. The reason prototypes need to be fast is that the design is not finished. Because the geometry lives in a program rather than a die, a revision is an edit and a re-cut — not a tool rework with the cost and delay that implies.
The prototype is made like the production part. Where the part will eventually be stamped, the prototype is normally laser cut and bent, which is a different process. That is worth knowing rather than hiding: it means the prototype validates the geometry, not the production process. Where it matters, we will tell you which characteristics a prototype cannot prove.
Engineering response in three hours. Drawings are reviewed by the people who will run the job. Most prototypes come back with a design change that removes cost or a feature that cannot be made as drawn — which is precisely the point of a prototype.
How to prototype a metal part
There are three practical routes, and the right one depends on which characteristics you are trying to prove.
Prototyping routes
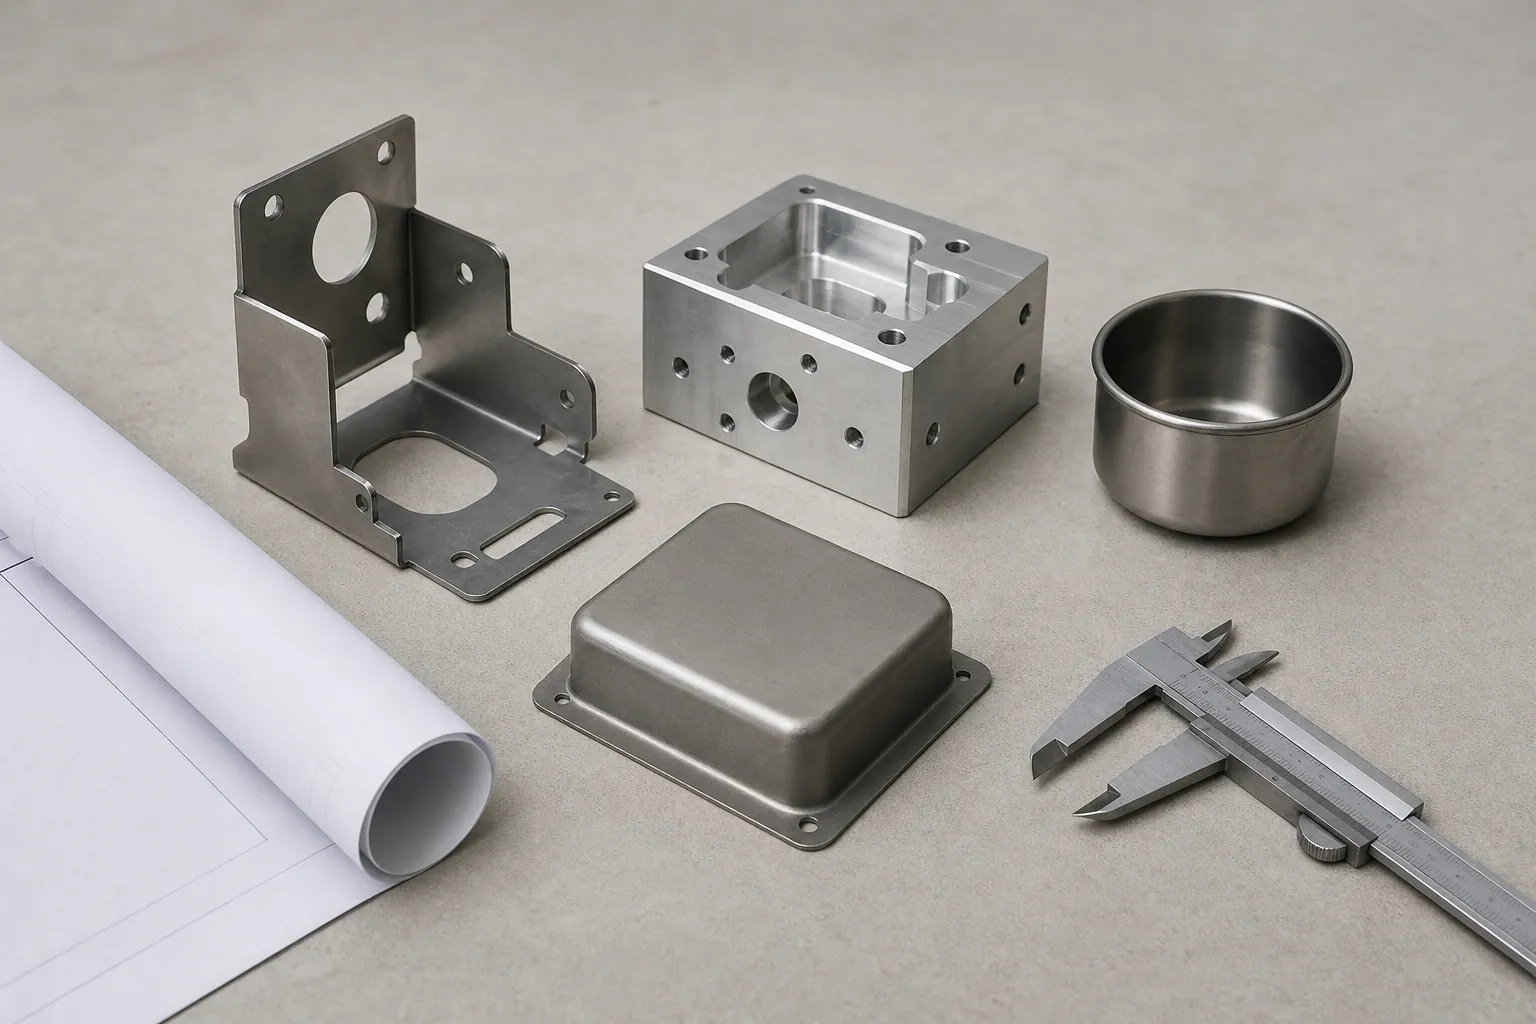
Laser cutting and bending — The default for sheet metal parts. The flat profile is cut with no tooling and formed on a press brake, which suits brackets, panels, enclosures and chassis, and validates fit and form in the real material. See laser cutting and sheet metal bending.
CNC machining — Where the part has a functional feature: a bore that a shaft must run in, a face a seal sits on, or a three-dimensional geometry that forming cannot produce. Machining holds ±0.005 mm, which is what makes it the route for proving tolerance rather than shape. See CNC machining.
Stamping from a temporary or soft die — Where the production process itself is what has to be proven — the strip layout, the springback, the burr condition. This costs more and takes longer than the two routes above, so it is normally only done once the geometry is settled and the volume is committed. See custom metal stamping.
Deep drawing for hollow forms — Where the prototype has to be a cup, can or seamless enclosure rather than a folded part, drawing is the process that produces the geometry at all. See metal deep drawing.
Prototype assembly — Where the point of the prototype is the built unit rather than the individual part, the components are made and then assembled and inspected as a unit. See assembly services. Once the design is frozen, see high-volume production for the volume end of the same service.
Why tooling-free prototyping is cheaper than it looks
| Factor | What it means commercially |
|---|---|
| No die to cut | The largest single cost of a new part is deferred until the design stops moving |
| Revision is an edit | A change costs a re-cut, not a tool rework |
| Real material | The prototype is made in the specified grade, not a substitute, so form and fit are meaningful |
| Real process for the critical features | Machined tolerances are proved by machining, not approximated |
| Production-representative documentation | First article inspection and CMM reporting from the prototype onwards |
| No minimum order | One piece is a valid order — the prototype is not subsidised by a batch you do not need yet |
Common prototyping scenarios
Design validation — A bracket, panel or housing cut and bent to check fit against the parts it will meet, in the real material and thickness.
Functional testing — Where the prototype has to perform: a machined component at final tolerance, tested under load before the design is committed.
Customer approval samples — A physical part for a customer or an internal sign-off, supplied with a first article inspection report so the approval is on measured dimensions rather than appearance.
Pre-tooling verification — The stage before a stamping die is cut, where the geometry is confirmed by laser cut and bent parts so the die is built once rather than corrected.
Fit and interference checks on assemblies — Multiple components made and test-assembled so that interfaces are proved before production tooling exists.
When a prototype is the wrong approach — if the part’s only requirement is a flat profile with clearance holes at high volume, prototyping is a formality and a die will be needed regardless; and if the design has to change with every use, fabrication rather than tooling is the right production route, not a temporary one.
How our rapid prototyping service works
1. Send the model or drawing. STEP, STP, SLDPRT, DXF, DWG or PDF, with the material and the function of the part. Tell us what the prototype has to prove — fit, strength, tolerance or appearance — because that decides which process route is right. Engineering responds within 3 hours on working days.
2. Route selection and DFM review, free. We check bend radii against the material, hole-to-bend clearances and minimum feature sizes, and confirm which route will actually validate what you are testing. Where a feature cannot be made as drawn, you hear it before the parts are cut rather than after.
3. Material. The prototype is made in the specified grade where available, so form and fit are meaningful rather than approximate. Material is verified against the mill certificate.
4. Manufacture. Laser cutting, bending, machining or drawing as the route requires, all in the same plant.
5. Deburring and finishing. Edges are deburred as standard; plating, anodising or coating can be applied where the prototype has to represent the finished part.
6. First article inspection and shipment. A first article inspection report and, where specified, a CMM dimensional report ship with the prototype.
Prototyping capabilities and specifications
| Parameter | Capability |
|---|---|
| Tooling required | None for cutting, bending and machining routes |
| Tolerances | ±0.005 mm machined; forming tolerances on cut and bent parts |
| Materials | Carbon steel, stainless steel (301/304/316L), aluminium (5052/6061), copper, brass, galvanised and pre-coated strip |
| Routes | Laser cutting and bending; CNC machining; deep drawing; assembly |
| Surface finishes | Zinc plating, powder coating, anodising, passivation, deburring, heat treatment |
| Minimum order quantity | None — from 1 piece |
| Engineering response | ≤3 hours on working days |
| Quality system | ISO 9001:2015, registration 34025Q30296R0S |
| Records supplied | First article inspection, CMM reports, EN 10204 material certificates |
| Plant | 15,000 m², 6 production lines, 85 employees |
Frequently asked questions about rapid prototyping
How fast can I get a metal prototype?
It depends on the route and the quantity, not on a single published figure. A flat cut and bent part from a completed drawing is the fastest case because no tooling is involved. Machined parts depend on programming and setup, and drawn parts depend on whether tooling is needed. Send the file with the material and the quantity and we will give you a date rather than an average.
Will my prototype be made the same way as the production part?
Often not, and it is worth being clear about it. If the production route is stamping, the prototype is normally laser cut and bent, which validates geometry, fit and form but not the stamping process itself. Characteristics such as burr height, die springback and strip layout can only be proven on production tooling. If those matter for your approval, tell us and we will say what the prototype can and cannot demonstrate.
Can you make a single piece?
Yes. There is no minimum order quantity on prototyping, and one piece is a normal order. That is a direct consequence of using processes that need no tooling — the cost of a one-off is the material, the machine time and the setup, not a share of a die.
Do I get inspection documentation with a prototype?
Yes. A first article inspection report ships with prototype work as standard, and a CMM dimensional report is available where you specify which dimensions to report. Having measured documentation from the prototype onwards means the approval is based on dimensions rather than on appearance, and the same reporting continues into production.
What if the prototype reveals the design cannot be made as drawn?
That is what the prototype is for, and finding it here is far cheaper than finding it on a die. Our DFM review normally catches those issues before the parts are cut — bend radii that the material cannot take, a hole too close to a bend, a sharp internal corner in a pocket, or a tolerance that no process will hold. When it does come up in the parts, the fix is a drawing revision and a re-cut rather than a tool rework.
Get a prototype quoted
Send the model or drawing with the material, the quantity and what the prototype needs to prove. You will get a route recommendation, a DFM review and a price — normally within one working day. See how we price metal fabrication, or use the RFQ form.
Related capabilities
- Custom laser cutting — flat profiles with no tooling
- Sheet metal bending — 3,200 mm CNC press brake
- CNC machining — ±0.005 mm for functional features
- Metal deep drawing — hollow forms and seamless enclosures
- Assembly services — prototype units built and inspected
- High-volume production — what happens once the design is frozen
Related solutions and resources
Prototyping is the first order, not the last. These are the pages that follow it:
- CNC machining — the tightest-tolerance prototyping route
- Custom laser cutting — flat prototype parts without tooling
- Metal stamping — where the part goes once the design is fixed
- High-volume production — the volume stage after sign-off
- CNC machining parts — worked examples from production
- Quality and inspection — first-article inspection on a CMM
See how a prototype order turned into a production conversation: Canada case study.
Standards referenced
- ASTM International — material and test standards
- NIST — measurement and dimensional metrology reference