
1. Pre-Processing Preparation
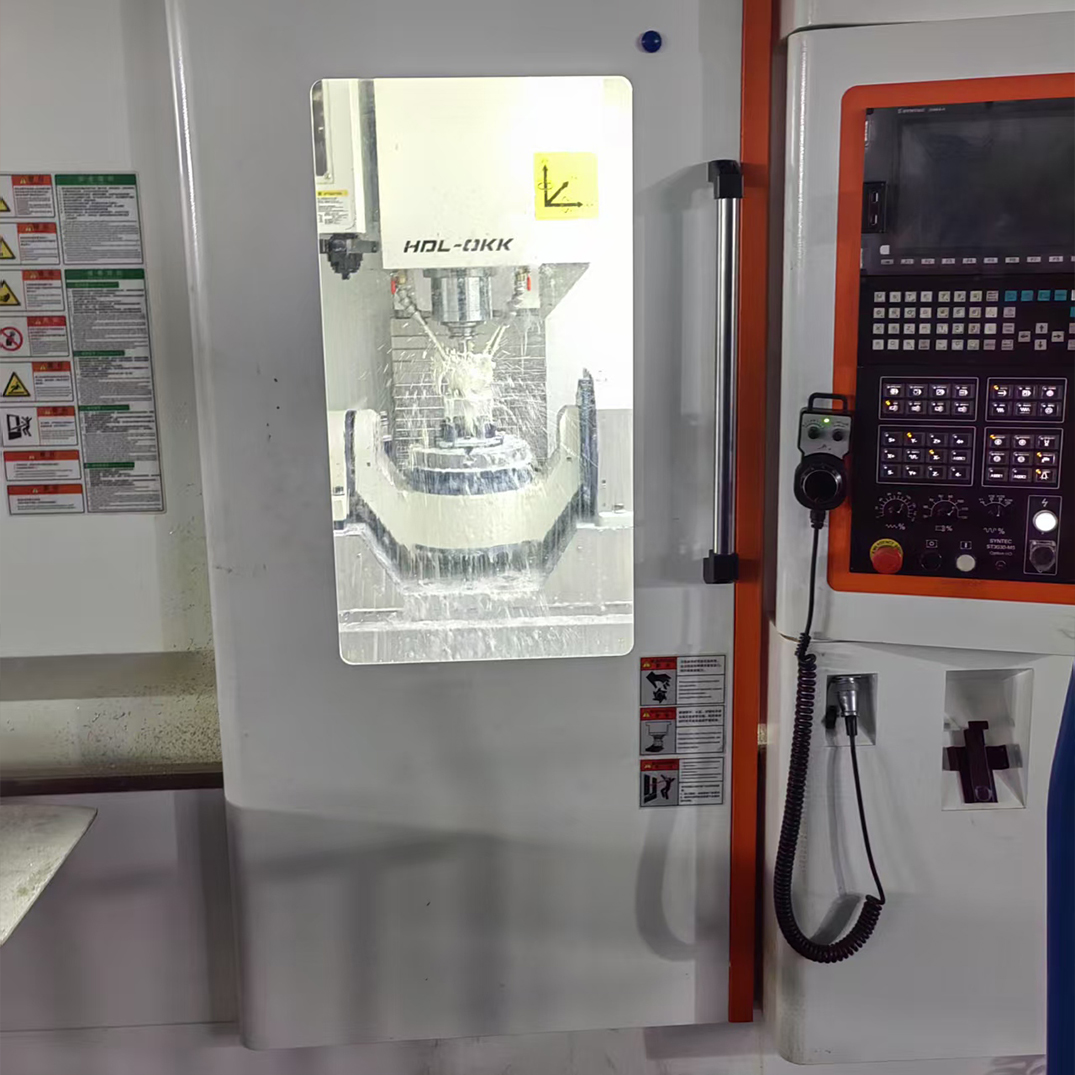
Machine Inspection and Warm-Up Before initiating any CNC operation, thorough equipment checks are vital. Ensure all components—such as bearings, motors, and fasteners—are secure and functional.Preheating the machine, as recommended by manufacturers, stabilizes thermal conditions, minimizing errors caused by temperature fluctuations.Program Simulation and Dry Runs Validate CNC programs using simulation software to detect coding errors. Conduct dry runs (without material cutting) to verify toolpaths, avoid collisions,and confirm alignment with design specifications.2. Workpiece Clamping and Positioning
Proper clamping prevents displacement during machining. Use precision fixtures and alignment tools (e.g., dial indicators) to secure workpieces.For complex parts, ensure the fixture design avoids interference with toolpaths and maintains accessibility.Multi-axis machines benefit from standardized coordinate systems to unify programming and operational benchmarks.3. Tool Selection and Maintenance
Material-Specific Tools Choose tools based on workpiece material (e.g., carbide for hardened steel, coated tools for alloys) and geometry.Regularly inspect for wear—excessive tool wear compromises surface finish and dimensional accuracy.Optimal Cutting Parameters Adjust spindle speed, feed rate, and depth of cut according to material properties. For example:- Hard materials (e.g., titanium): Lower speed, higher feed, shallow cuts.
- Soft materials (e.g., aluminum): Higher speed and deeper cuts. Real-time monitoring of vibration and temperature helps refine parameters.
4. Machining Process Control
Quality Assurance Through Data Analysis Leverage sensors and software to track metrics like cutting force, tool wear, and dimensional deviations.Historical data analysis identifies trends, enabling proactive adjustments to improve yield and reduce scrap.In-Process Monitoring Monitor machining sounds and load meters. Abnormal noises or sudden load spikes often indicate tool breakage or misalignment, requiring immediate intervention.5. Post-Processing and Quality Control
Dimensional Verification Use precision instruments (e.g., CMMs, micrometers) to validate critical dimensions, surface roughness, and geometric tolerances. Implement statistical process control (SPC) for batch consistency.Machine Calibration and Maintenance Regularly calibrate CNC axes and spindle alignment. Lubricate moving parts and replace worn components to sustain accuracy.6. Safety and Compliance
Adhere to strict safety protocols:- Wear PPE (safety glasses, gloves).
- Avoid manual adjustments during operation.
- Clear debris using specialized tools (not hands). Maintain a clean workspace to prevent contamination and accidents.
Key facts
| Process | CNC machining of metal components |
| Preparation | Machine inspection, warm-up, program simulation and dry runs |
| Workholding | Precision fixtures and alignment tools to prevent displacement |
| Tooling | Material-specific tools, such as carbide for hardened steel and coated tools for alloys |
| Verification | Critical dimensions checked on CMMs and micrometers, with SPC for batch consistency |
| Safety | PPE required, with no manual adjustment during operation |
Frequently asked questions
What preparation happens before CNC machining starts?
Before any cutting begins the machine is inspected and warmed up, because preheating stabilises thermal conditions and reduces errors caused by temperature changes. Programs are then validated with simulation software and run dry, without material, to check toolpaths, avoid collisions and confirm alignment with the design.
How do you choose cutting tools and parameters?
Tools are matched to the workpiece: carbide for hardened steel and coated tools for alloys. Cutting parameters are then set by material, with hard materials such as titanium run at lower speed, higher feed and shallow cuts, while softer materials such as aluminium take higher speed and deeper cuts. Vibration and temperature are monitored so the parameters can be refined.
How are finished CNC parts checked?
Critical dimensions, surface roughness and geometric tolerances are validated on precision instruments such as CMMs and micrometers, and statistical process control is applied for batch consistency. CNC axes and spindle alignment are calibrated regularly, and worn components are replaced, so accuracy is maintained rather than assumed.
Related capabilities
We produce parts of this type with CNC machining.
Related pages


