
Sheet metal fabrication tolerances depend on the process, not on a single house figure. As a working guide: machining holds ±0.005 mm on features that require it, sheet metal fabrication tolerances on formed features sit near ±0.1 mm, and laser cutting holds approximately ±0.05 mm on a cut profile.
Key facts: sheet metal fabrication tolerances
| CNC machining | ±0.005 mm on features that require it, on an HDL-OKK DMU38 five-axis machining centre |
| Sheet metal forming | Approximately ±0.1 mm on formed features, with tighter limits achievable where the drawing specifies them |
| Laser cutting | Approximately ±0.05 mm positional accuracy on a cut profile |
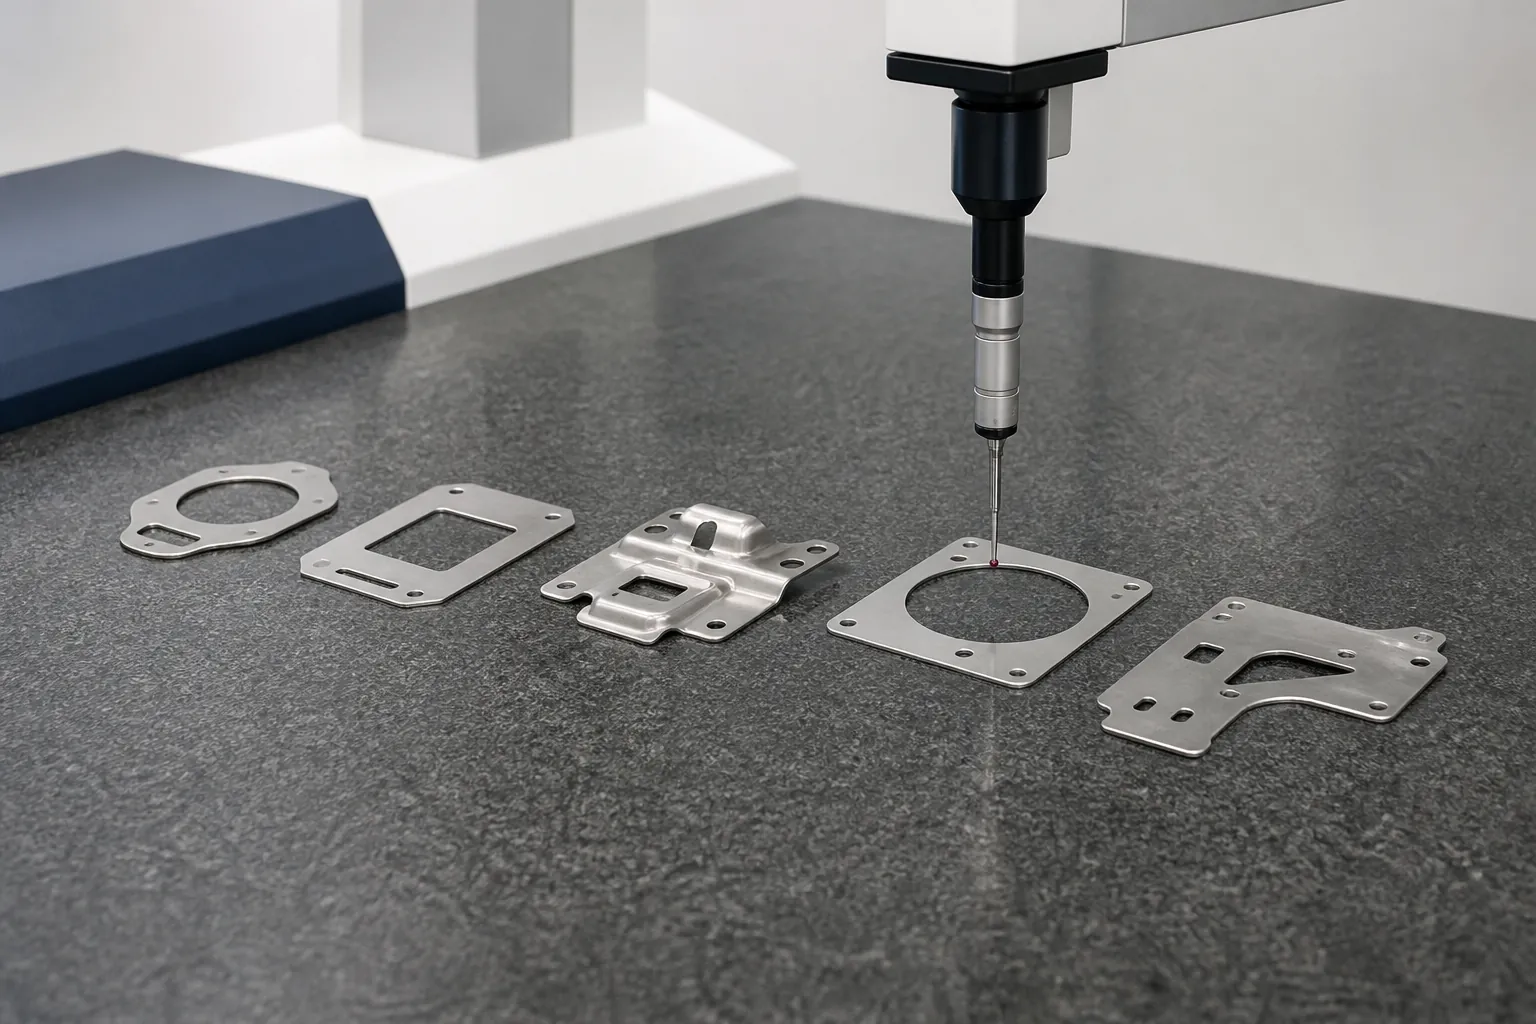
| Measurement | Coordinate measuring machine with a stated measuring accuracy of ±0.002 mm |
Why a cutting tolerance is not a machining tolerance
This is the distinction that costs buyers most. A laser cut profile is accurate in position, but the process does not create a machined surface, hold a bore diameter or produce a flatness callout. Specifying ±0.005 mm on a laser cut edge asks for something the process does not deliver — and paying for it results in extra machining operations rather than a tighter cut.
The practical rule: a laser cut profile holds a fraction of a millimetre, and anything tighter is machined afterwards. Bores, bearing seats, threads and faces that must be flat belong to CNC machining, whether or not the blank started on the laser. Saying which features are critical is the single most useful thing you can put on a drawing, because it puts tight limits where they function and nowhere else.
Where forming tolerances actually come from
Formed features inherit error from three places: the flat blank, the bend deduction, and springback. Springback varies with material grade and thickness, which is why bend deduction has to be calculated against the real material rather than left at a default. For that reason we inspect the formed part rather than only the flat blank — twist and angle error are measurable after forming, not before.
Bend radius matters here too. An inside radius below the material thickness risks cracking on the outside of the bend, and stainless steel is the more sensitive grade because it work-hardens. Our metal bending page covers radii, reliefs and hole-to-bend clearances.
How tolerances are verified
First article inspection runs on production jobs, and 100% of critical dimensions are verified before shipment using a coordinate measuring machine with a stated measuring accuracy of ±0.002 mm. Results ship as CMM dimensional reports. Measurement practice follows NIST reference.
For context on what a tolerance costs, see how metal fabrication prices are calculated and equipment and capacity.
Frequently asked questions
What tolerances can you hold?
Machining holds ±0.005 mm on features that require it, formed sheet metal features sit near ±0.1 mm, and laser cutting holds approximately ±0.05 mm positionally on a cut profile. Tolerance depends on the process, so tell us which features are critical and we will confirm what is achievable.
Can laser cutting hold the same tolerance as machining?
No. A laser cut profile is accurate in position, but the process does not create a machined surface, hold a bore diameter or produce a flatness callout. Specifying ±0.005 mm on a laser cut edge asks for something the process does not deliver, and paying for it results in extra machining operations rather than a tighter cut.
How are tolerances verified before shipment?
First article inspection runs on production jobs, and 100% of critical dimensions are verified before shipment using a coordinate measuring machine with a stated measuring accuracy of ±0.002 mm. Results ship as CMM dimensional reports, so you receive the measured values rather than a pass stamp.